The 55 mm bore of the 32000 Series Tapered Roller Bearings is the 32011: 55 mm bore, 90 mm outside diameter, 23 mm wide. This page gives the dimensional row from the table, the shaft and housing fits that suit it, the internal clearance to expect and the mounting, lubrication and failure notes that go with the type.
55 mm Bore Dimensional Row (ISO 355 / DIN ISO 355 / GB/T 297)
| Designation | Bore d (mm) | Outer diameter D (mm) | Assembled width T (mm) | Width B (mm) | Width C (mm) | Contact angle a (deg) | Chamfer r min (mm) |
|---|---|---|---|---|---|---|---|
| 32011 | 55 | 90 | 23 | 23 | 17.5 | 14 | 1.5 |
What a 32000 Series Tapered Roller Bearings Does
The rollers, the cone raceway and the cup raceway are all cones whose apices meet on the bearing axis, so the rollers roll without sliding and the bearing carries very heavy combined radial and axial load. Radial load generates an axial reaction that must be taken by a second, opposed bearing — tapered roller bearings are specified, mounted and adjusted in pairs.
Combined radial and axial load, with the axial component taken in one direction only. Radial load on a tapered roller bearing also generates an axial reaction of its own, so the bearing has to be opposed by a second one and the pair adjusted to an endplay or a preload on assembly.
Speed at 55 mm Bore
No limiting speed is tabulated for this product. Where speed matters, the figure to work to is the one the bearing supplier states for the exact design, cage and lubricant supplied — not a family value.
Shaft & Housing Fit for a 55 mm Seat
With the inner ring rotating under a load whose direction is fixed, the inner ring sees a circumferential load and must be an interference fit, or it will creep on the shaft and fret it. The outer ring sees a point load and takes a transition or clearance fit so that it can shift slowly and spread the wear — and so that one of the two bearings on the shaft is free to take up axial expansion.
| Shaft, light load (P ≤ 0.06 C) | j6 |
|---|---|
| Shaft, normal load (P = 0.06–0.12 C) | k5 or k6 |
| Shaft, heavy or shock load (P > 0.12 C) | n6 |
| Housing — Axial displacement of the outer ring required | H7 |
| Housing — Normal load, outer ring may still shift | J7 |
| Housing — Normal to heavy load, quiet running, outer ring not displaceable | K7 |
ISO 286-2 tolerance grades, applied per the conventional bearing seat recommendations of ISO 1132-2 and DIN 5425-1, for a SOLID STEEL shaft in a cast iron or steel housing. A hollow shaft, a thin-walled housing or a light alloy housing needs a tighter fit than these, because the seat itself deflects.
Radial Internal Clearance at 55 mm Bore
This type is specified by PRELOAD, not by a clearance group. The rings are set against one another on assembly — by a ground spacer, by a matched set, or by drawing a nut up to a measured endplay — and the resulting axial setting decides the stiffness, the running accuracy and the heat generated. Ordering a "C3" version of this bearing asks the wrong question: the equivalent decision here is light, medium or heavy preload, or a specified endplay.
Abutment Shoulder & Fillet Radius for 55 mm
The chamfer dimension r min for this size is 1.5 mm. That figure is a limit on YOUR machining, not just on the bearing: the fillet radius in the corner of the shaft or the housing must be smaller than the bearing's corner radius, or the ring seats on the fillet instead of on the shoulder face and is loaded on its corner.
| Chamfer dimension r min (from the table) | 1.5 mm |
|---|---|
| Maximum fillet radius on the shaft or housing | 1.5 mm |
| Shaft shoulder must exceed | 58 mm diameter |
| Housing shoulder bore must be under | 87 mm diameter |
The two shoulder figures are the geometric floor and ceiling: a shoulder outside them fouls the corner radius instead of bearing on the ring face. The practical values sit inside them — the shoulder must contact the ring face over a useful area without touching the seal, the cage or the opposite ring, and it must still leave room for a puller when the bearing is dismounted. Take the working da and Da from the abutment table for the bearing; the ring shoulder height they are built on is not a boundary dimension and is not in this table.
Mounting a 55 mm Bore 32000 Series Tapered Roller Bearings
The ring that carries the rotating load takes an interference fit; the ring under a stationary point load takes a transition or clearance fit so that it can creep slowly and spread the wear, and so that one ring is free to take up axial expansion. With a rotating shaft under a fixed load direction, that means an interference fit on the shaft and a looser fit in the housing. Press only against the ring being fitted — force driven through the rolling elements leaves brinell marks in the raceway before the bearing has run a revolution.
At a 55 mm bore the interference is small enough that a cold press or a light hydraulic press is normally enough; heating the bearing in an induction heater or an oil bath to 80–100 °C above the shaft is the alternative, and never above 120 °C for a standard-stabilized bearing. Keep the heated bearing pressed against the shoulder while it cools, because it shrinks axially as well as radially.
This bearing is separable, which makes mounting easier and mis-mounting easier too: fit each ring to its own seat separately, and do not let the two halves be swapped between bearings once they have run — the raceways wear as a matched pair.
Lubrication & Relubrication
Oil is the usual lubricant here, because this type is used where the load, the speed or the heat generated is beyond what a grease charge can carry away. Oil bath, oil mist, circulating oil and jet lubrication all take heat out of the bearing as well as separating the surfaces, and the viscosity has to be selected at the OPERATING temperature — a viscosity chosen at 40 °C when the bearing runs at 90 °C is not the film thickness the calculation assumed.
Failure Modes and What They Look Like
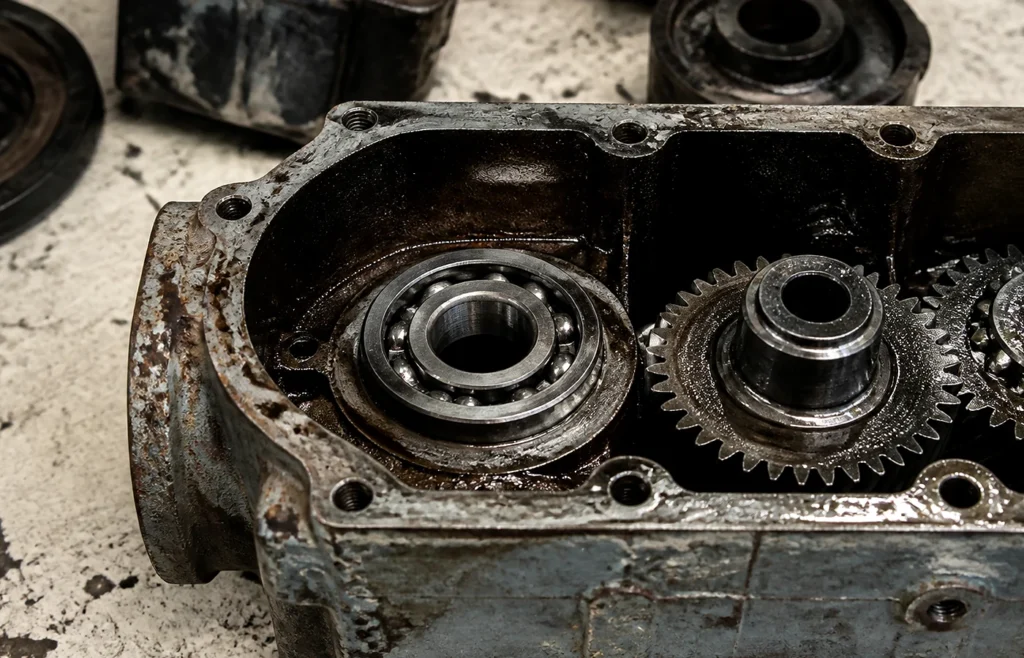
- Subsurface fatigue (spalling) — a flake of raceway lifts out and the bearing gets noisy and rough. This is the failure the L10 life calculation predicts — if it arrives near the calculated life the bearing did its job, and if it arrives early the load, the fit or the lubrication was not what the calculation assumed.
- Inadequate lubrication — a polished, then discoloured, then torn raceway, running hot with a darkened grease. It is the most common cause of early failure by a wide margin, and the interval, not the grease, is usually what was wrong.
- Contamination — dents in the raceway with raised edges, then premature spalling from those dents. Wear particles, casting sand and washdown water all do it; sealing and filtration are what prevent it.
- False brinelling and fretting — evenly spaced dull marks at ball or roller pitch, produced by vibration while the shaft is stationary — a machine that travels on a truck, or a standby pump beside a running one. It is not caused by overload and cannot be cured by fitting a bigger bearing.
- Edge loading at the roller ends — wear or spalling concentrated in a band at one end of the roller path. It means misalignment or deflection: line contact has no tolerance for angular error, which is what the crowned profile can only partly correct.
Where NOT to Use a 32000 Series Tapered Roller Bearings
- Do not mount a tapered roller bearing singly or leave it unadjusted. It generates its own axial reaction under radial load, and an unopposed or unset pair either runs with damaging endplay or is preloaded into overheating.
- Do not mix a cup and a cone from different bearings, or swap them between bearings after running. The two halves wear as a matched pair, and cup and cone from different sets do not share the same rated geometry.
- Do not adjust the setting on a cold bearing and forget the temperature rise. The endplay set on assembly shrinks as the shaft heats; a cold zero-endplay setting can become a hot preload.
Stepping Up or Down from 55 mm
Within the same series, the next bore up in this series is 60 mm and the next bore down is 50 mm. Changing bore changes the shaft, so it is the last thing to change: when the calculated life at 55 mm is short, the first move is to a heavier diameter series at the SAME bore — the 6300 envelope instead of the 6200, for instance — which raises the rating without touching the shaft. The second is to change type: a roller bearing carries far more radial load than a ball bearing of the same envelope.