Application guide for KR Series Stud Type Track Rollers to DIN 5429 / ISO 1206. The core duty of the type is carrying a high radial load in the smallest radial section of any rolling bearing — a needle assembly is only a few millimetres larger in diameter than the shaft it runs on. A long, small-diameter roller has a large contact length and almost no radial height, so the bearing fits where the space between shaft and housing is a few millimetres and a ball bearing simply will not go. The typical industries, the specification checklist, mounting practice and the exclusion cases are set out below. This series is catalogued from 16 mm to 52 mm roller outside diameter; the full table of boundary dimensions is further down the page.
Typical Applications for KR Series Stud Type Track Rollers
The machine positions and sectors where this type is specified:
- Automotive transmissions: idler gears, shafts and thrust positions throughout a gearbox where radial space is tight everywhere.
- Pumps and compressors: eccentric drives and rocker arms with heavy radial load in a small envelope.
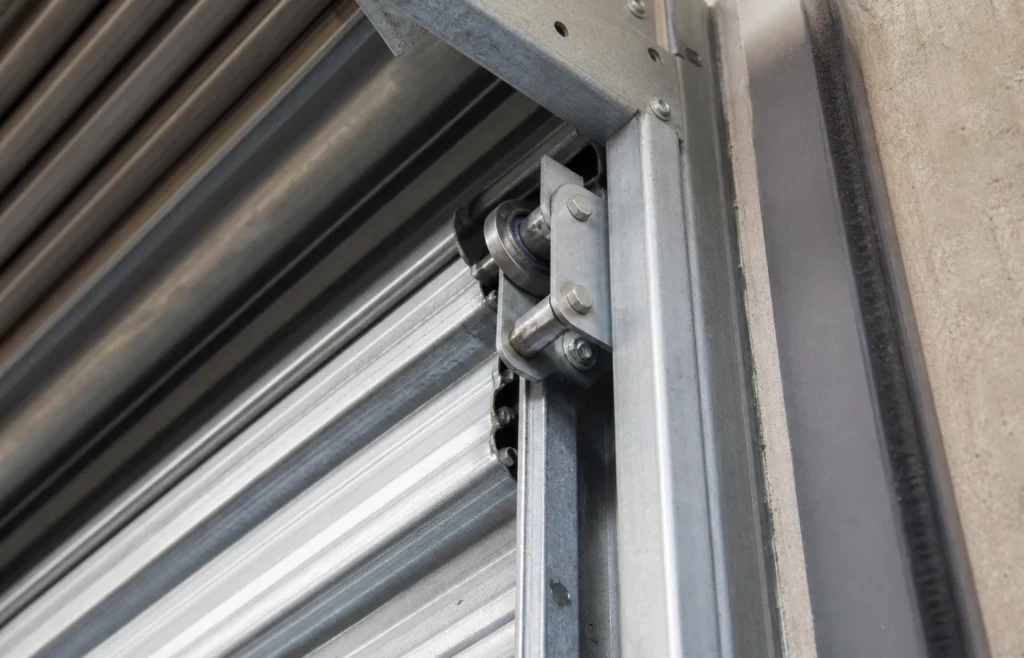
- Cam and track roller mechanisms: cam followers and track rollers where the outer ring runs directly on a track or a cam.
- Steering and control mechanisms: oscillating pivots that must be compact and low-friction.
- Maintenance and repair (MRO): replacing a failed bearing where the original designation, clearance group and sealing have to be matched exactly.
How to Specify KR Series Stud Type Track Rollers for Your Application
- Roller outside diameter: Start from the roller outside diameter the shaft or housing gives you — this series is catalogued from 16 mm to 52 mm — then check the outer diameter and width against the space available. The boundary dimensions are fixed by the standard, so they are the same from any manufacturer; the load ratings and limiting speeds are not, and belong to the specific bearing being supplied.
- Stud and outer ring form: Specify the stud thread (for KR types), the crowned or cylindrical outer ring form, and the sealing. A crowned outer ring tolerates a slight track misalignment; a cylindrical one does not.
- Bearing form: Three forms, three different specifications. A drawn cup (HK, BK) is a thin pressed outer ring that takes its finished size from the housing bore — so the housing tolerance is part of the bearing. A machined ring type (NA, RNA, NKI) has a rigid outer ring and, in the NA and NKI forms, its own inner ring. A cage-and-roller assembly (K) has no rings at all and runs directly on hardened shaft and housing raceways.
- Raceway hardness and finish: Where the bearing runs directly on the shaft or the housing, that surface is a raceway: harden it to 58–64 HRC with adequate case depth and grind it to a fine finish. This is not an installation detail, it is half the bearing.
- Designation and suffixes: State the complete designation including every suffix. The base number gives the type and the boundary dimensions; the suffixes carry the sealing, the cage, the clearance group, the tolerance class and any special execution — and two bearings whose base numbers match but whose suffixes differ are not interchangeable.
- Clearance and tolerance: State the running clearance or fit class the assembly requires, together with the tolerances of the mating parts that produce it. For this type the clearance is created by the parts around the bearing rather than being built into it, which is precisely why it has to be written down.
- Sealing arrangement: This type is supplied open, so the sealing belongs to the housing around it. Specify the shaft seal, flinger or labyrinth that will keep the lubricant in and contamination out — with an open bearing, the sealing arrangement, not the bearing, decides how long it survives its environment.
- Cage material: State the cage. Pressed steel is the default and suits most duties; machined brass takes shock, high temperature and poor lubrication better and is used in large and heavily loaded bearings; polyamide is quiet, light and low-friction but has a temperature limit of about 120 °C and is attacked by aged oil. The cage is not a detail — it is the component that most often sets the real temperature limit of the bearing.
- Shaft and housing fit: Specify the seat tolerances, not just the bearing. The rule is that the ring which rotates relative to the load direction takes the interference fit: for a rotating inner ring under normal radial load the shaft seat is typically k5 or k6 with the housing bore H7, and where the outer ring rotates the interference moves to the housing (N7 or P7) with a clearance fit (g6) on the shaft. Heavier loads and hollow shafts move the fits tighter. A correctly chosen bearing in the wrong fit fails anyway — too loose and the ring creeps and frets its seat, too tight and the interference consumes the internal clearance and the bearing runs preloaded.
- Standard: Boundary dimensions are to DIN 5429 / ISO 1206. Quoting the standard on the order guarantees the mounting dimensions are interchangeable between suppliers — it does not standardize load ratings, limiting speeds or internal design, which remain manufacturer-specific.
Mounting & Assembly Practice
- Press a drawn cup with a mandrel bearing on the marked, closed end face only. The cup wall is thin enough that force applied anywhere else deforms it, and a deformed cup has no clearance left.
- Support the housing during pressing and lead the cup in square: a cup started at an angle will not straighten as it enters.
- Check the housing bore tolerance before ordering, not after fitting. The drawn cup conforms to the bore, so an oversize bore leaves the bearing loose and an undersize bore closes the running clearance.
- Where a cage and roller assembly runs directly on the shaft, verify the shaft hardness and surface finish on the actual part rather than assuming the drawing was followed.
Common Selection Mistakes with KR Series Stud Type Track Rollers
- Running a needle assembly directly on an unhardened or soft shaft. The rollers indent the surface within hours and the bearing is then running on a corrugated raceway.
- Ignoring the housing bore form tolerance for a drawn cup, which is what actually sets the bearing clearance.
- Choosing a drawn cup for a heavy shock load. The pressed section that makes it compact is also what limits it — a machined ring type carries far more.
- Sizing this bearing from the boundary dimensions alone. Load ratings and limiting speeds are manufacturer-specific for this series and are deliberately not published here — take them from the catalog of the bearing actually being supplied and calculate the life against them.
Where KR Series Stud Type Track Rollers Are Not the Right Choice
- Not for a track that is soft or unhardened — the roller then wears the track instead of running on it.
- No axial capacity at all in a radial needle bearing. Thrust must be taken by a shoulder, a thrust washer or a separate thrust needle assembly.
- Not where the shaft or housing cannot be hardened and ground to raceway quality — use a type with its own inner and outer rings instead.
- No misalignment tolerance. A long roller on a line contact loads its end the moment the shaft tilts, and needle rollers are the longest rollers in the catalog relative to their diameter.
- Not for high speed. The rollers are guided loosely and slide against each other and the cage more than in other types.
- No axial capacity: the shaft has to be located by another bearing, a shoulder or a retaining ring.
- This type will not tolerate misalignment. The rolling or sliding contact is a line, so a fraction of a degree of tilt moves the whole load onto the end of the contact and the stress concentration there is what fails the bearing.