
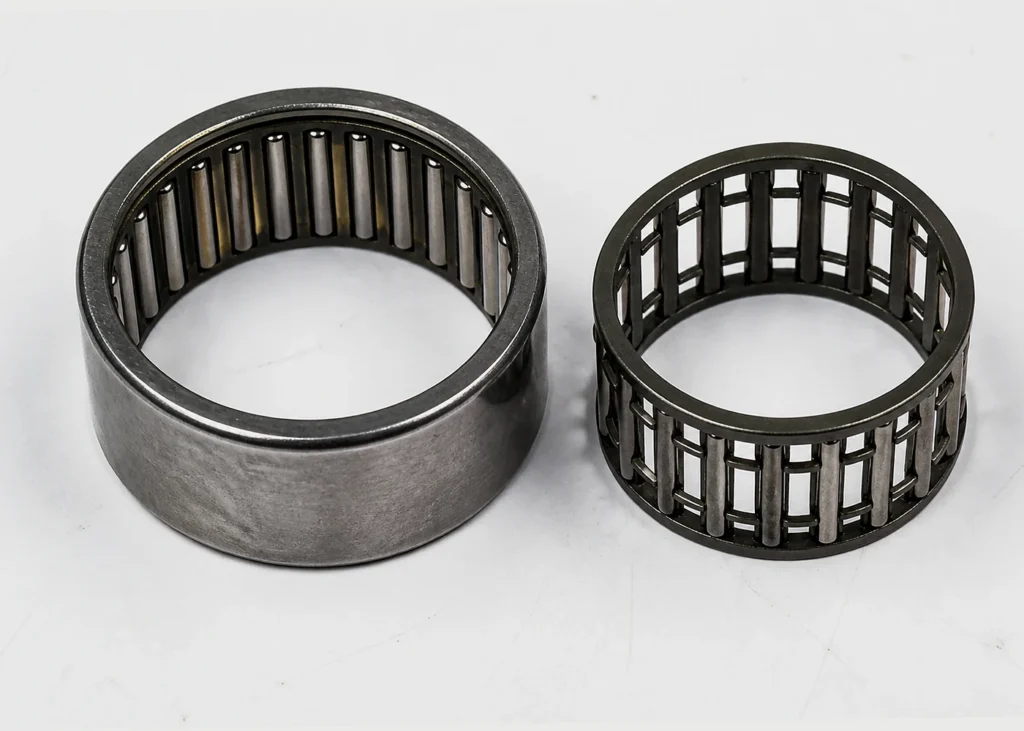
Manufactured to ISO 3245 / DIN 618-1, HK-2RS Series Sealed Drawn Cup Needle Roller Bearings are needle roller bearings supplied by Bushing Bearings. Every designation in the series is listed with its boundary dimensions; the interactive half-section drawing redraws itself for whichever size you select.
What Are HK-2RS Series Sealed Drawn Cup Needle Roller Bearings?
HK-2RS Series Sealed Drawn Cup Needle Roller Bearings are needle roller bearings defined by ISO 3245 / DIN 618-1. They are selected by bearing designation and the dimensional characteristics shown below. Material, cage and sealing are specified separately from the designation and are covered further down this page.
Materials & Cage
Drawn cups are case-hardened low-carbon steel, formed and then carburized, and they run directly on the shaft — so the SHAFT is a bearing raceway and must be hardened to 58 to 64 HRC and ground to h5 or h6. Machined rings and needles are through-hardened GCr15 / 100Cr6. Where the shaft cannot be hardened, specify a variant with an inner ring instead.
Typical Applications
Planet gears, universal joints, connecting rods, pumps and automotive transmissions, where the radial section available for the bearing is the limiting dimension. Read the full application guide for HK-2RS Series Sealed Drawn Cup Needle Roller Bearings →
Pricing
HK-2RS Series Sealed Drawn Cup Needle Roller Bearings are supplied to order. Pricing starts from approximately US$1.10 per piece for standard sizes in case-hardened steel, without an inner ring; final pricing depends on size, material, finish and order quantity (MOQ applies). Submit your exact configuration with the quote form above.
Specifying the HK-2RS Series Sealed Drawn Cup Needle Roller Bearings
If the shaft is already fixed, go straight to the size: 20 mm bore, 25 mm bore, 30 mm bore and 35 mm bore. Each of those pages repeats only the row that matters for that bore, with the fit and clearance notes underneath it.
Where the environment decides the specification rather than the load, the material pages are the ones to read: Pressed Steel Cage, Polyamide Cage and Machined Brass Cage. Each states what the grade survives, and what choosing it costs in load capacity or temperature range.
For the machines and duties this type is actually specified for, see where hk-2rs series sealed drawn cup needle roller bearings are fitted.
Manufactured in our own plant
This bearing is forged, hardened, ground, superfinished and clearance-set in-house. The stages below are where its tolerance class, its internal clearance and its noise grade are actually decided.
-

01 Forging & turning
GCr15 bar and tube is cut, heated and forged into ring blanks, then turned to leave a uniform grinding allowance. Forging rather than machining from solid keeps the grain flow following the raceway, which is the surface that eventually fails.
Blank dimensions and grinding stock checked at set-up and per shift.
-
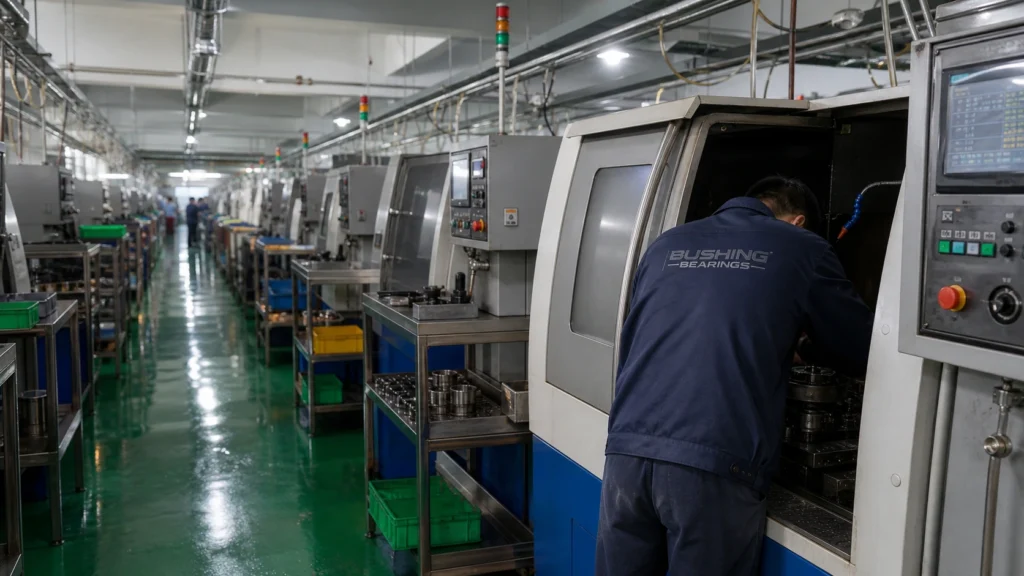
02 Heat treatment
Through-hardening brings GCr15 / 100Cr6 to 58–64 HRC; carburizing case-hardens 20CrMnTi where the section is heavy or the load is shock. Rings are then stabilized so they hold size in service rather than growing in the housing.
Core and surface hardness per lot; retained austenite and dimensional stability to the ordered temperature class.
-
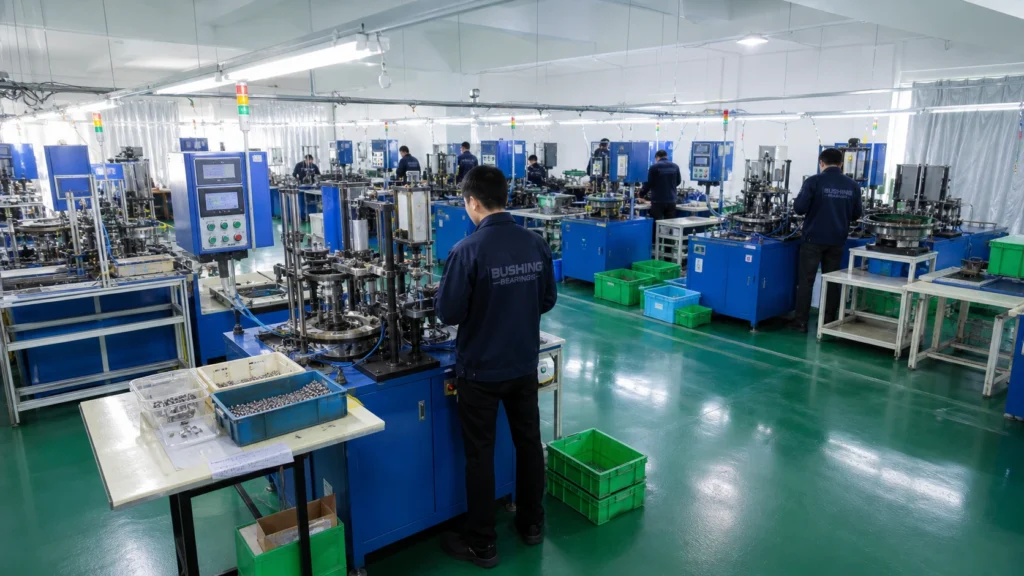
03 Raceway grinding
Faces, bore, outer diameter and raceway are ground in sequence on separate machines. This is where the tolerance class is created: P0, P6, P5 or P4 is a grinding outcome, not a sorting outcome.
Bore and outer diameter deviation, raceway roundness and face runout measured to ISO 492 on every setup.
-
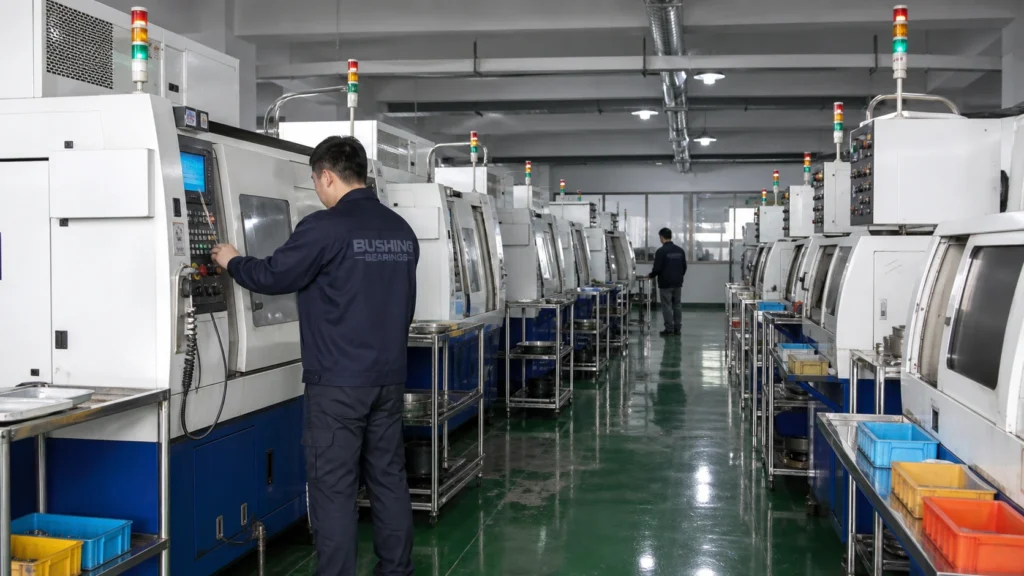
04 Honing & superfinishing
The ground raceway is honed to remove the grinding lay and bring surface roughness down to a fraction of a micrometre. Raceway finish is what decides whether a lubricant film forms, and therefore what decides bearing life far more than the load rating alone.
Surface roughness Ra and waviness measured per lot.